Key Quality Requirements in Pipeline Anti-Corrosion
efore steel tubes enter 3LPE, 3LPP, or liquid epoxy coating systems, surface quality directly impacts the long-term adhesion and cathodic disbondment resistance of the protective layer:
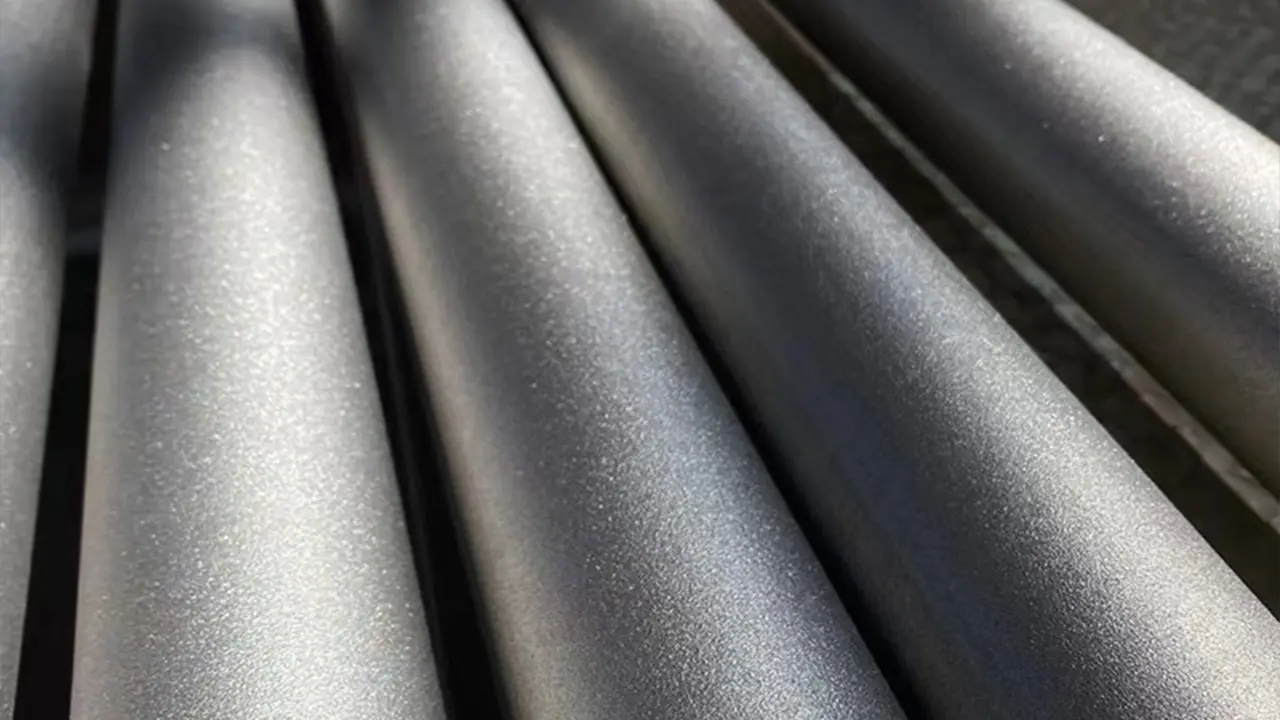
SA 2.5 Cleanliness: Complete removal of mill scale, rust, oxidation, and surface oils according to ISO 8501-1.
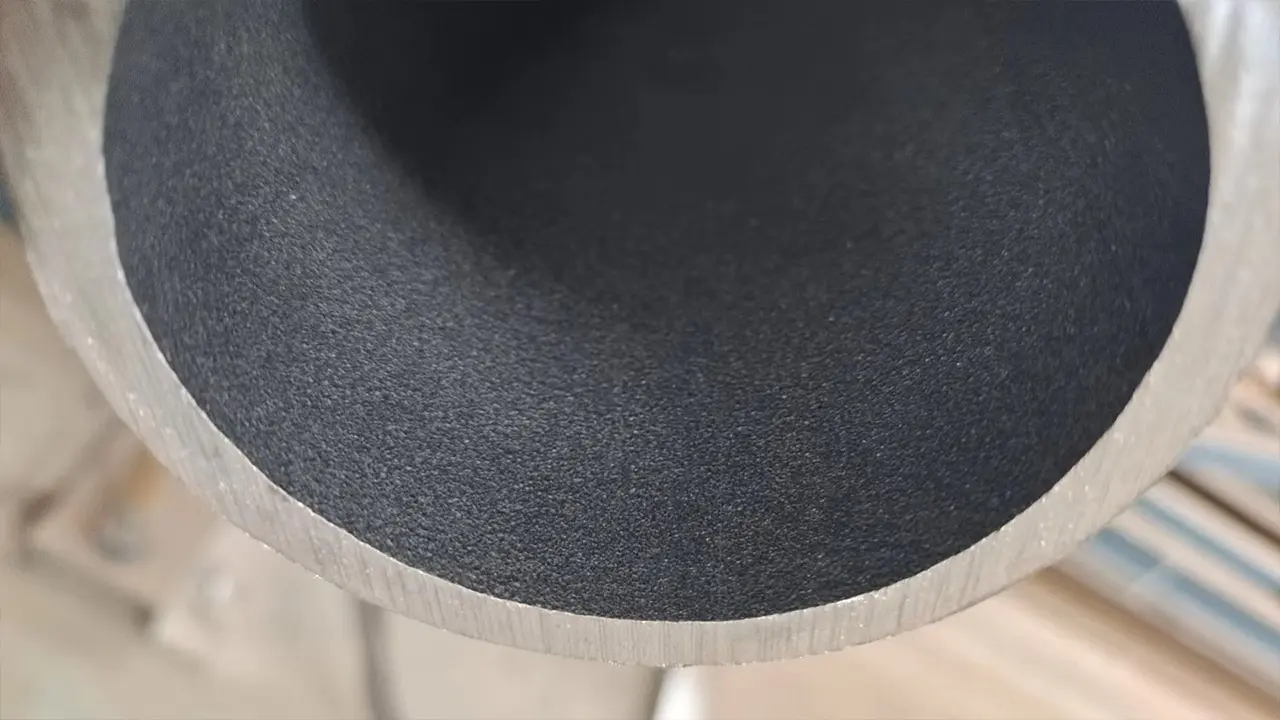
Optimal Anchor Profile (50 to 90 microns): Creating the exact mechanical interlocking roughness required for fusion-bonded epoxy (FBE) primers.
Dust & Moisture Control: Eliminating residual fine dust particles to prevent micro-blistering under the coating film.
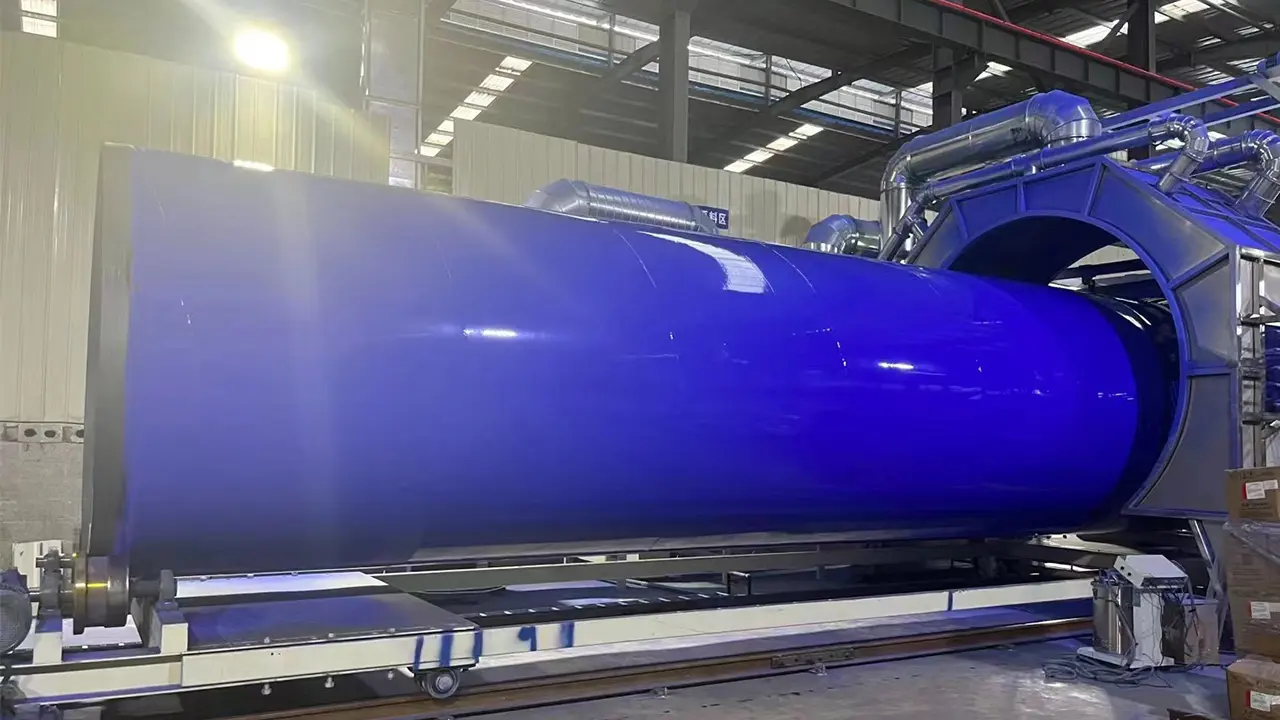
External Tube Prep: Overcoming Coverage Shadowing
Outer wall surface processing requires continuous rotational movement to prevent uneven blast patterns across round geometries.
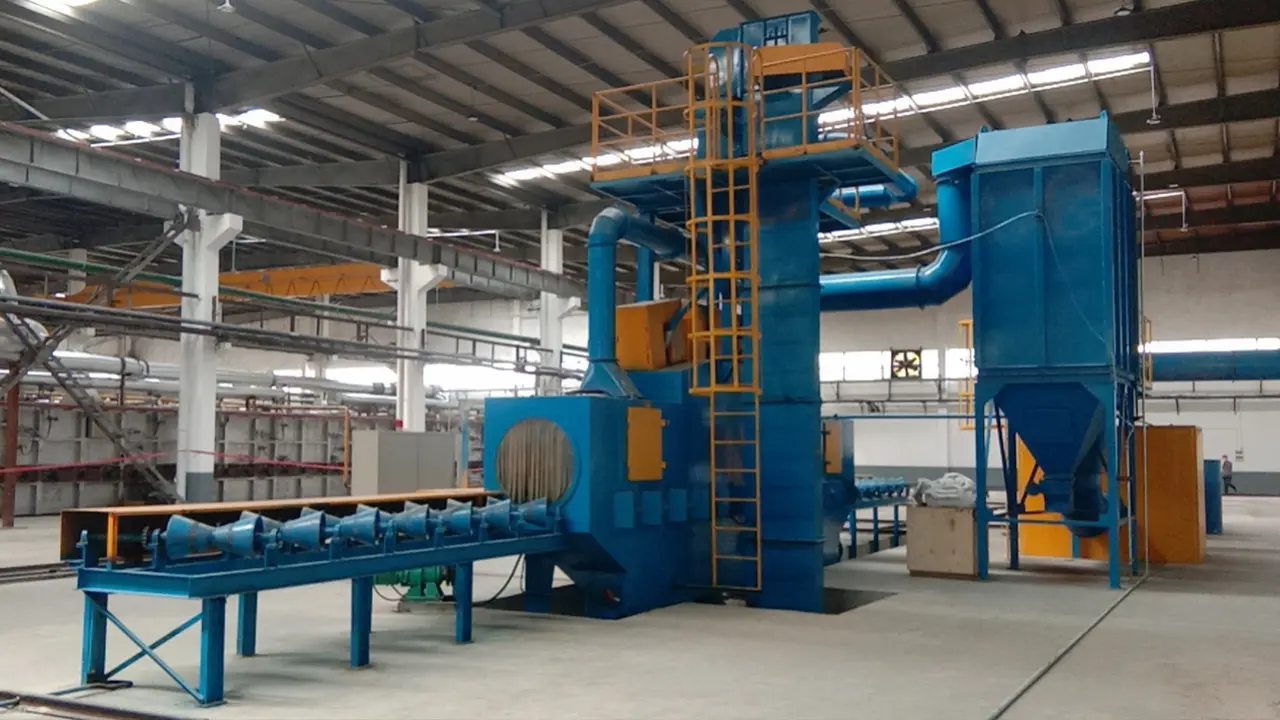
Process Motion: Pipe Entry -> Helical Compound Movement (Linear Forward + Axial Rotation) -> Blast Chamber Processing.
Helical Conveyance Mechanics: Skew-roll drive systems impart simultaneous linear travel and axial rotation, ensuring every square centimeter receives uniform blast energy.
Controlled Velocity & Abrasive Blend: High-efficiency blast wheels launch a balanced mix of steel grit and shot to cut the profile without imbedding contaminants.
Internal Cavity Cleaning: Evacuation and Access
Internal pipe walls present strict accessibility boundaries where traditional centrifugal blast wheels cannot fit.
Pneumatic Deflection Lances: For small-to-medium diameters (100mm to 600mm ID), pressurized lance units deploy 360-degree deflector nozzles during controlled retraction passes.
Motorized Internal Cars: For large tubes (600mm+ ID), internal mobile units carry oscillating spray arms or specialized compact blast heads directly into the cavity.
Positive Air Sweep & Vacuum: Integrated air blow-out modules ensure spent grit and loose dust are continuously evacuated out of long tube sections.
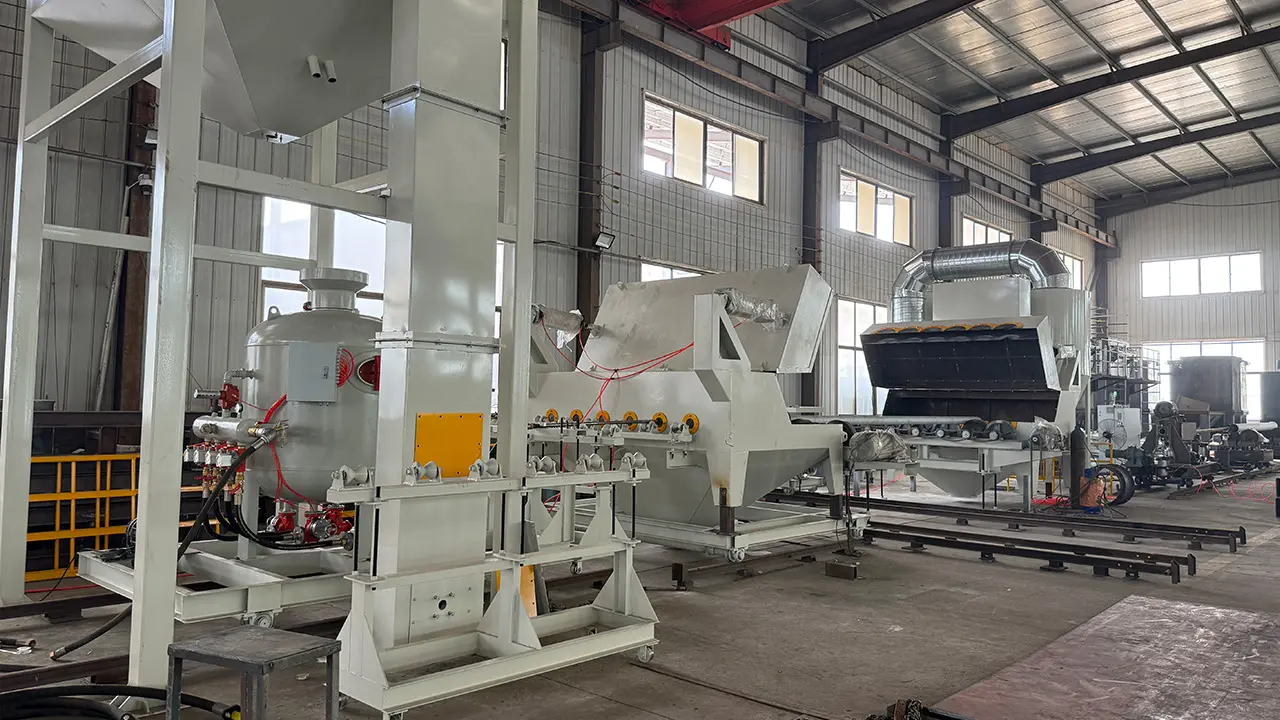
Heavy-Duty System Integration by HQAMUR
High-Manganese Protection: Chamber hot-zones incorporate heavy rolled MN13 manganese steel armor to resist continuous grit abrasion over multi-shift operations.
Closed-Loop Media Separation: High-efficiency air-wash separators cleanse re-circulated abrasive, removing fines and dust before re-entry into the blast wheels.
Centralized Line Control: Loading mechanisms, skew-roll drives, and internal lances are linked via Siemens PLC interfaces for single-operator oversight.